- +8618937185591
- +8618937185591
- ec19@zkcorp.com
- +8618937185591
Project Introduction
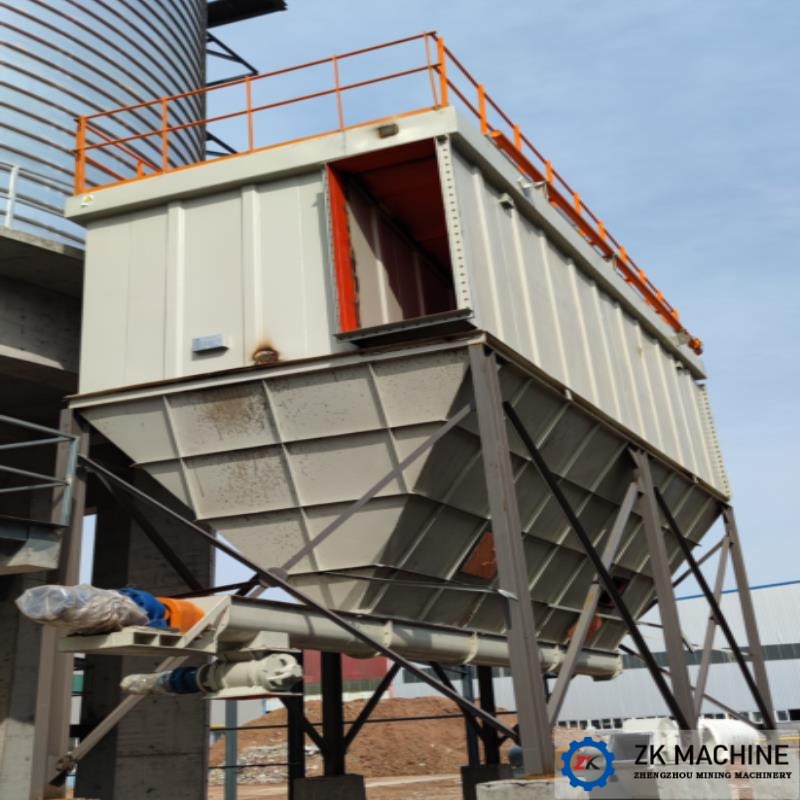
A customer of a copper ore processing project in Central Asia needed a dust collector system for the crushing section of its copper mine. Since the dust in this section is explosive and highly abrasive, the customer required the dust collector system to be explosion-proof. In addition, the project also required a supporting air compressor system, thermal insulation and sound insulation for the pipelines, and lining materials at the pipe elbows to enhance wear resistance.
Project Solution
Based on the air volume requirements, the technical team of Henan Zhengzhou Mining Machinery Co., Ltd. carefully carried out the selection of the dust collector and made specialized designs targeting the explosion-proof characteristics:
Explosion-proof Design:
• Enlarging the angle of the ash hopper to effectively reduce material accumulation;
• Installing explosion-proof valves to ensure safe system operation;
• Adopting a high dust explosion-proof grade for both the motor and the electrical control system.
Wear Resistance, Thermal Insulation and Sound Insulation Design:
• Using 100mm thick rock wool for thermal and sound insulation;
• Fabricating the elbows with thickened steel plates and adding ceramic lining plates to improve wear resistance;
• Innovatively adopting a “backpack” structure for the elbows, filled with sand and gravel, to further enhance wear resistance.
Energy-saving Optimization:
Through professional calculations such as fluid dynamics, and by taking into comprehensive consideration the dust collection point data, pipeline length, and inlet/outlet dust concentration requirements, the technical team worked out the optimal fan selection scheme, which minimizes energy consumption while meeting the dust removal requirements.
Project Implementation
During the project implementation stage, Henan Zhengzhou Mining Machinery Co., Ltd. tailored and delivered a complete, safe, and stable explosion-proof dust collection system for the project. The system accurately implemented the preliminary plan in actual practice, with the following core implementation measures:
1. Full-process explosion-proof design — explosion-proof requirements were fully taken into account in every design stage, building a solid line of defense for safe production;
2. Optimized fan selection — the fan power was reduced as much as possible on the premise of meeting the operating conditions, balancing practicality and energy saving, effectively reducing noise, and greatly saving the customer’s investment cost;
3. Optimization of dust collection points and pipeline system — multiple requirements including wear resistance, thermal insulation, and sound insulation were comprehensively considered;
4. Precise drawings guiding installation — supported by the accurate design and layout drawings provided by our company, the on-site installation proceeded in an orderly manner, and the entire system was successfully connected and operated smoothly.
The project truly achieved a worry-free, labor-saving, and cost-saving experience for the customer.
Henan Zhengzhou Mining Machinery Co.,Ltd. has always maintained a professional technical team, excelling in customized design based on different customers’ actual working conditions and personalized needs. The smooth implementation of this project not only effectively solved the technical difficulties encountered by the customer during energy transition and equipment upgrading but also significantly reduced fuel costs for the customer, creating remarkable economic benefits and winning high recognition from the customer.
Fast, professional and reliablewe provide you with services throughout the product ...

Email
ec19@zkcorp.com

Whatsapp
+8618937185591
Fast, professional and reliablewe provide you with services throughout the product . you with services t